MWD / LWD & Downhole
Components for downhole tools, MWD/LWD equipment and surface drilling hardware, machined in the alloys the service calls for.
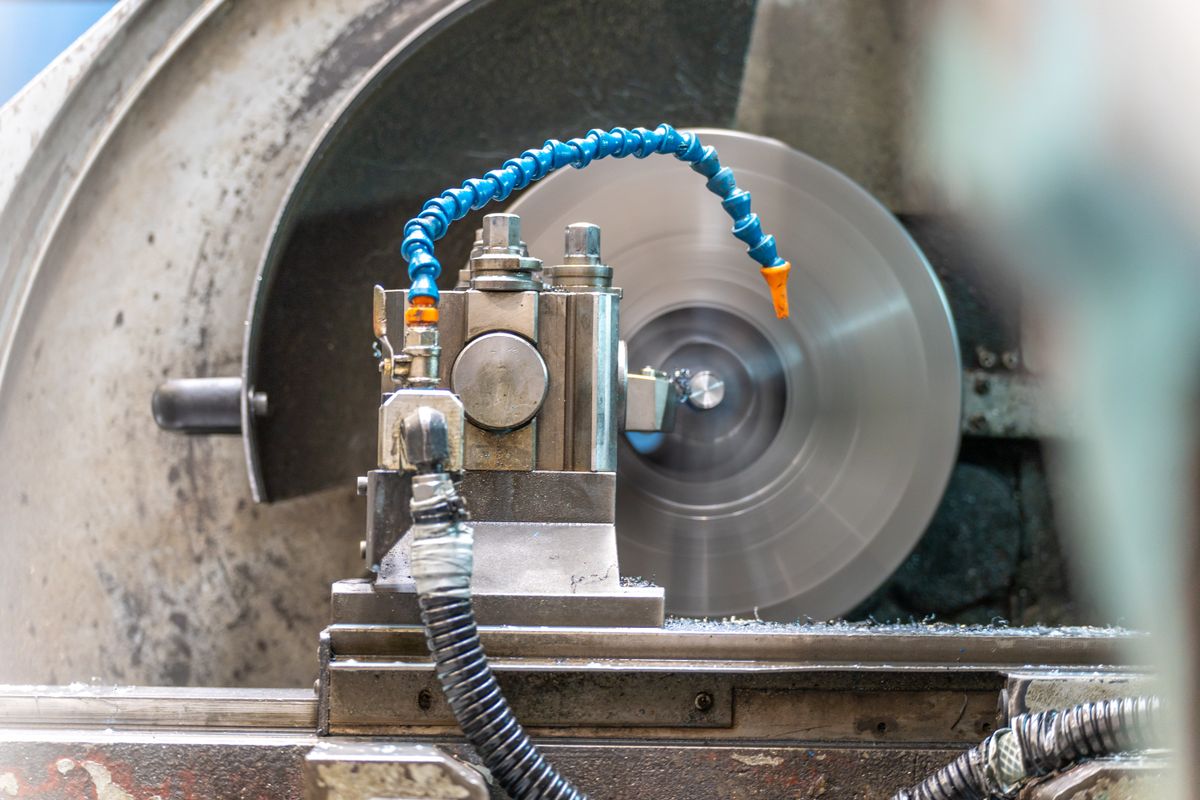
Components for downhole tools, MWD/LWD equipment and surface drilling hardware, machined in the alloys the service calls for.
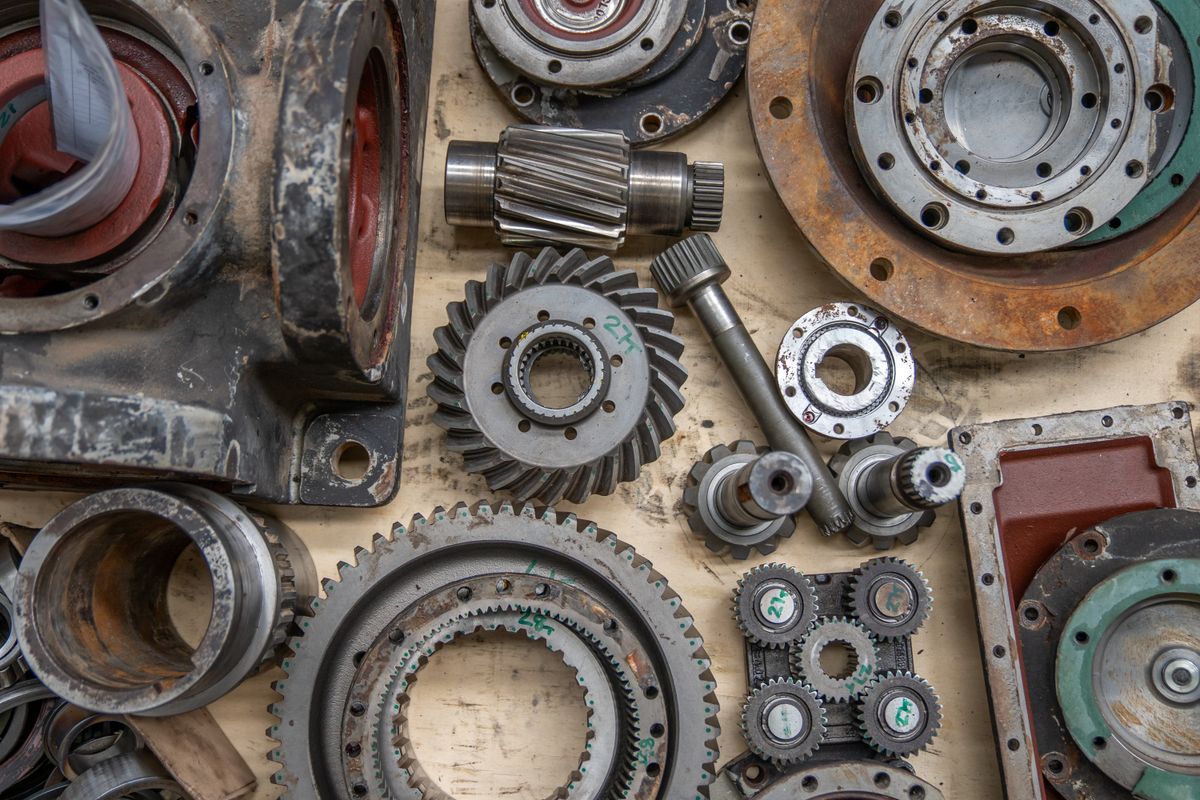
Downhole work punishes parts in ways a shop floor never sees: vibration at temperature, drilling fluid at pressure, and a tool body that has to survive being run in and out of a hole for years. The drawing usually reflects that experience. The machining has to respect it.
Most of what we make here is small to medium batch — sensor housings, flow sleeves, mandrels, connector bodies and thread subs. Beryllium copper and nickel alloys come up often, and the parts are usually non-magnetic or corrosion-critical.
What we make here
Typical work: traceable batches where the material certificate and the dimensional report travel with the parts.
How the work runs
Materials, equipment and inspection
Inconel 718 and 625, MP35N, 17-4PH, 4140, duplex stainless and C17200 beryllium copper. Threads are usually API or specified on the drawing; where a thread is not standard we cut to the drawing rather than substitute.
CMM for position and profile, thread gauges for API and UN threads, surface finish on sealing faces, and material certificates traceable to the heat number. NACE-related requirements quoted case by case.
Capacity
| Part family | Typical material | What decides the price |
|---|---|---|
| Sensor and electronics housings | BeCu C17200, 17-4PH | Wall thickness and non-magnetic verification |
| Flow sleeves and restrictors | Inconel 718, MP35N | Alloy machinability and bore tolerance |
| Mandrels and tool bodies | 4140, duplex | Length, concentricity and thread callout |
| Threaded subs and connectors | 4140, 17-4PH | Thread form, gauge class and pressure rating |
| Seal and O-ring grooves | 316L, BeCu | Groove finish and positional tolerance |
| Surface drilling hardware | 4140, 4340 | Size and batch, usually turned and milled |
Non-magnetic is a material property, not a machining one. If the drawing says non-magnetic, the certificate has to prove it — we check the response and record it.
Parts we have machined
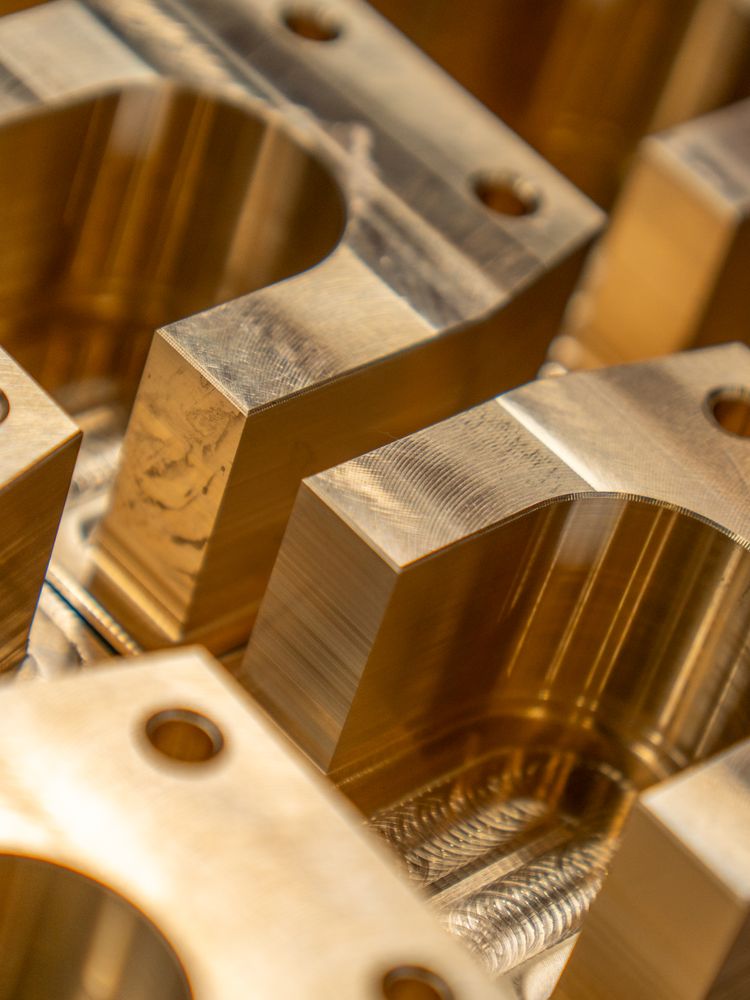
Where the money goes
Straight answers
Yes — C17200 is one of the materials we run regularly. It is machined with attention to dust control and tool wear, and parts are checked for magnetic response where the drawing calls for it.
API and premium connections are quoted from the drawing or the standard named on it. We confirm the thread form before cutting, because a substituted thread is not a small mistake downhole.
Yes, traceable to the heat number and issued with the parts. If the end user needs a specific mill or certification, say so at enquiry rather than after the material is cut.
Keep reading
Request a quotation
Industry fit is checked before the price is argued. Send the drawing with the service conditions and we will answer on both.