CNC Turning
Shafts, sleeves, connectors and threaded parts — turned to drawing, and milled in the same setup where the feature calls for it.
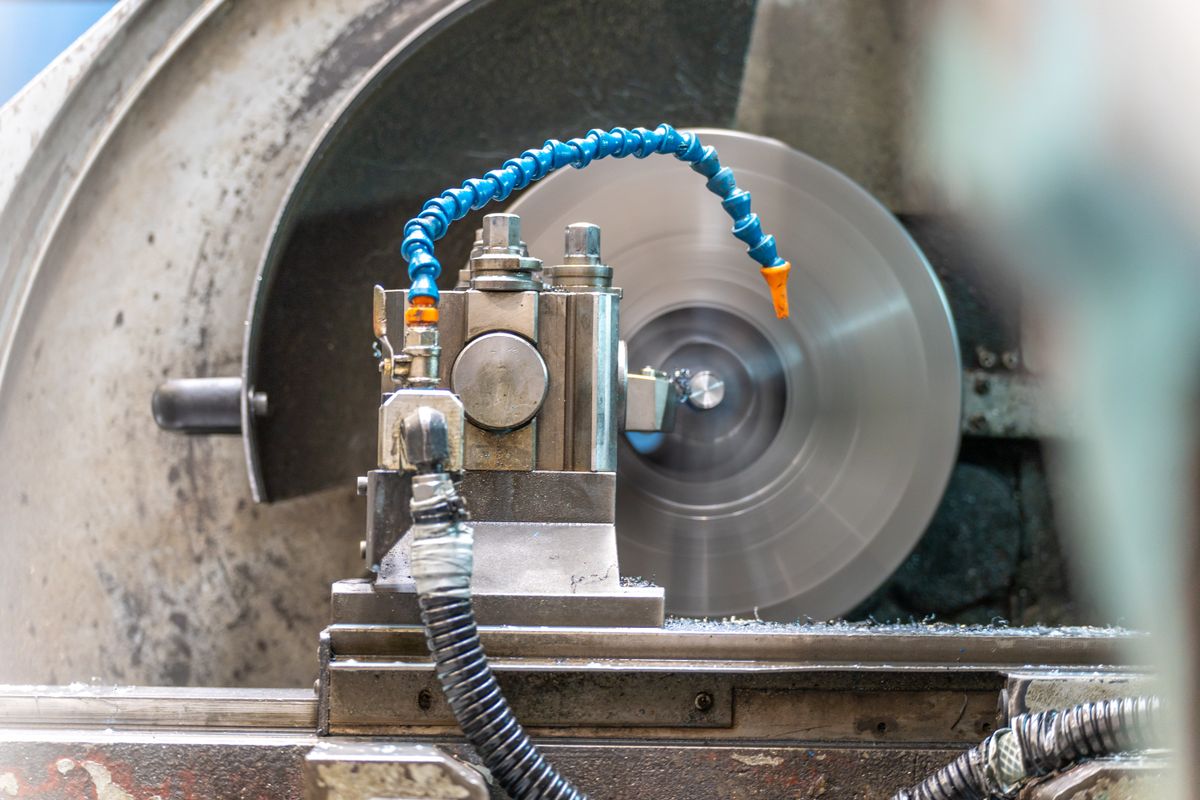
Shafts, sleeves, connectors and threaded parts — turned to drawing, and milled in the same setup where the feature calls for it.
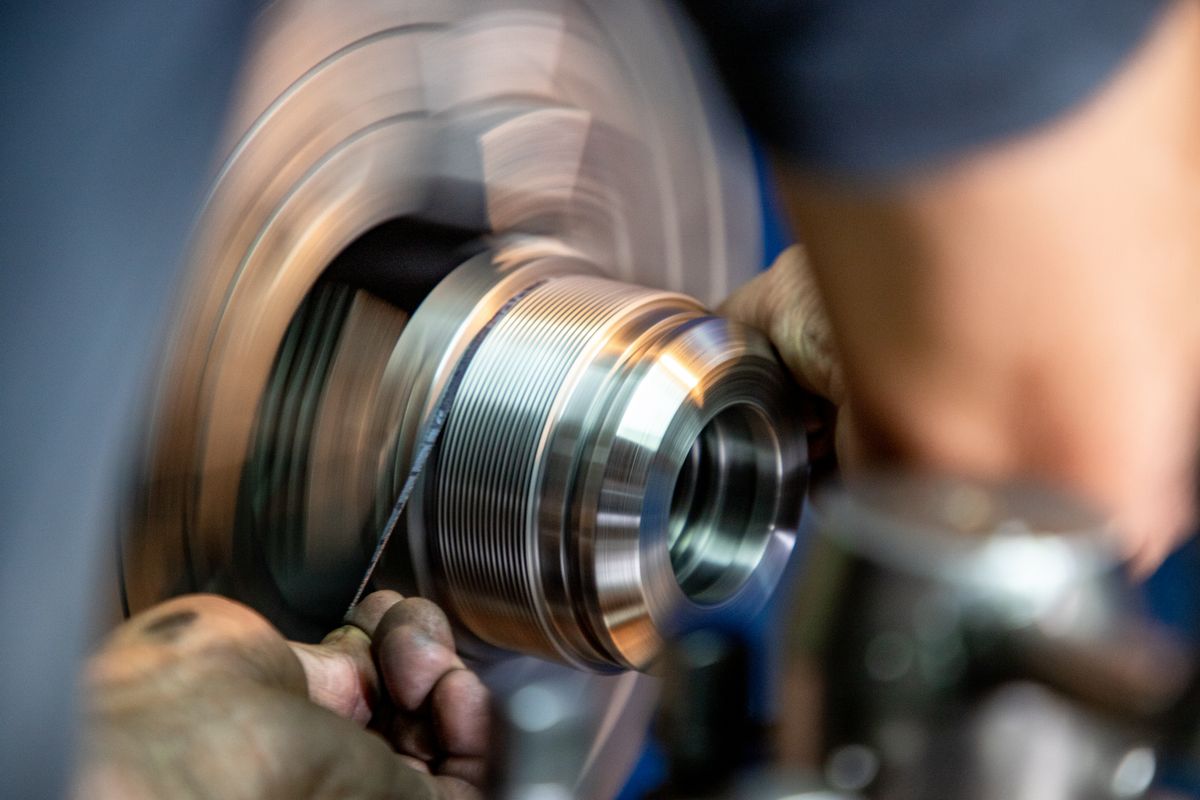
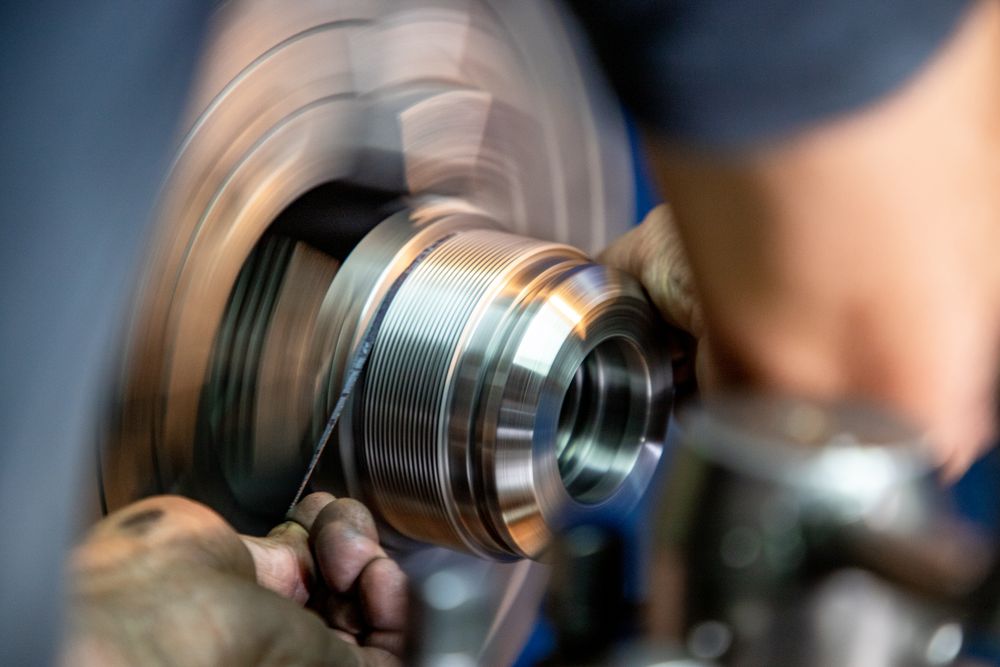
Turning is where most precision assemblies start. The department runs from simple pins and spacers to mill-turn work where bores, slots and cross-holes have to stay concentric with the main axis — and where a second operation would mean re-establishing datums you already controlled.
Because grinding, gear cutting and EDM sit in the same building, a turned part that needs heat treatment and a ground journal does not leave the floor between operations. The engineer who quoted it signs the inspection report.
What we make here
Typical work: small to medium batches where repeatability across the run matters more than the price of the first piece.
How the work runs
Materials, equipment and inspection
Carbon and alloy steels, stainless steels, nickel and high-temperature alloys, aluminium, brass and copper, titanium and engineering plastics — turned from bar, or from material you supply and we verify on receipt.
CNC lathes and mill-turn machines with live tooling for cross-holes and flats. Threads checked with go/no-go gauges, diameters with micrometers and bore gauges, profiles on the vision measuring machine.
Capacity
| Feature | Range | What to know |
|---|---|---|
| Max swing over bed | Ø420 mm | Larger diameters quoted with the chuck removed |
| Max turning length | 1,000 mm | Between centres, tailstock supported |
| Bar capacity | Ø5–51 mm | Bar feeder for unattended runs above 500 pieces |
| Live tooling | 6,000 rpm driven tools | Cross-holes, flats and slots in the same setup |
| Threads | M1.6–M64 · UN · BSP · NPT | API and premium connections quoted to the drawing |
| Roundness | 0.003 mm achievable | On a ground or hard-turned journal |
| Surface finish | Ra 0.4 µm as turned | Ra 0.2 µm where the part is subsequently ground |
Ranges are indicative. The envelope that matters is the one your part needs — send the drawing and we confirm the exact machine before quoting.
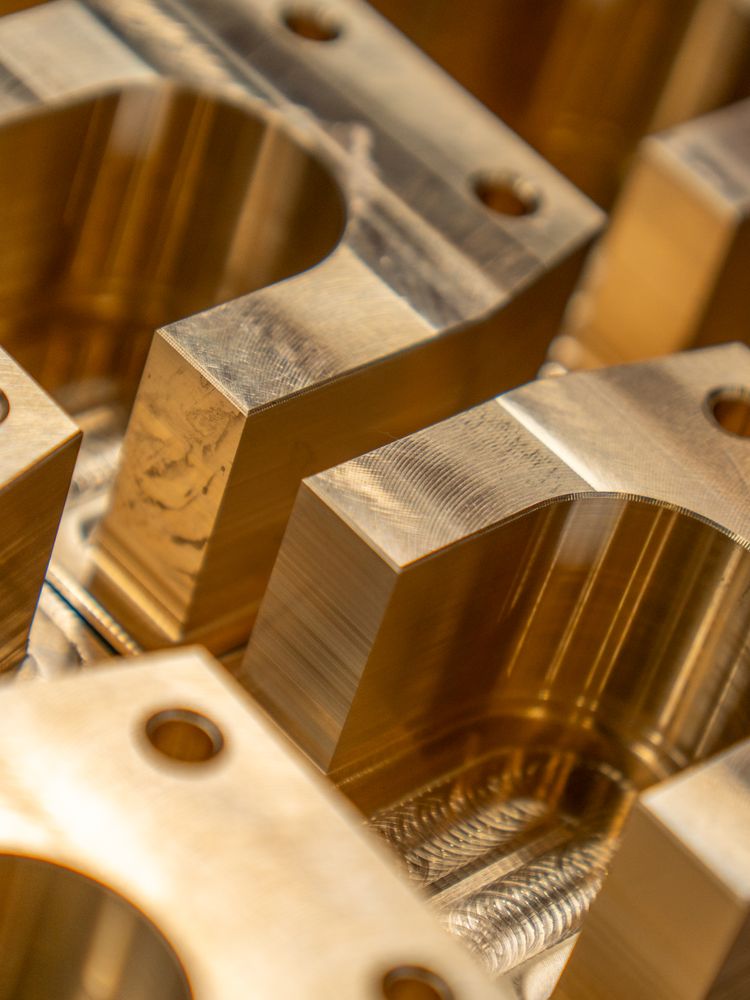
Parts we have machined
Where the money goes
Straight answers
The drawing, the material and grade, the quantity and the date you need the parts. If a critical feature is ambiguous we ask rather than assume — a one-line question now is cheaper than a rework later.
For straightforward parts, usually yes. We measure the sample, send you a drawing for approval, and machine against the approved drawing so both sides are working from the same document.
By machining as much as possible in one setup, and where that is not possible, by turning soft jaws or a fixture to the part rather than re-chucking on a scroll. Where the tolerance is tight, the outside diameter is ground after hardening.
Keep reading
Request a quotation
Tell us the part, the material and the quantity. An engineer reviews your drawing and replies within one working day — usually with a suggestion on how to make it cheaper.